

A Tier-2 machining shop in Manesar wins a new part number on a Friday. The customer wants a Level 3 PPAP submission with the first production lot, the plant has one quality engineer, and that engineer is already running the trial run for another part. The drawing is released, the route is confirmed, the gauges exist. What does not exist is the forty-odd pages of documentation that turn measured data into a package a checker will accept. That is the moment a supplier asks whether to build the pack in-house or hand the documentation to an outside desk.
- What does PPAP Desk actually do, and what does it never do?
- PPAP Desk versus in-house: the side-by-side comparison
- When is in-house PPAP the right call?
- When does the outsourced desk make sense?
- How does a PPAP Desk engagement run, day by day?
- What should a supplier ask before choosing either route?
- A decision rule a plant manager can use
- A worked example: the Friday nomination in Manesar
- Common mistakes when outsourcing PPAP documentation
- How to brief a PPAP desk so the pack comes back usable
- People also ask
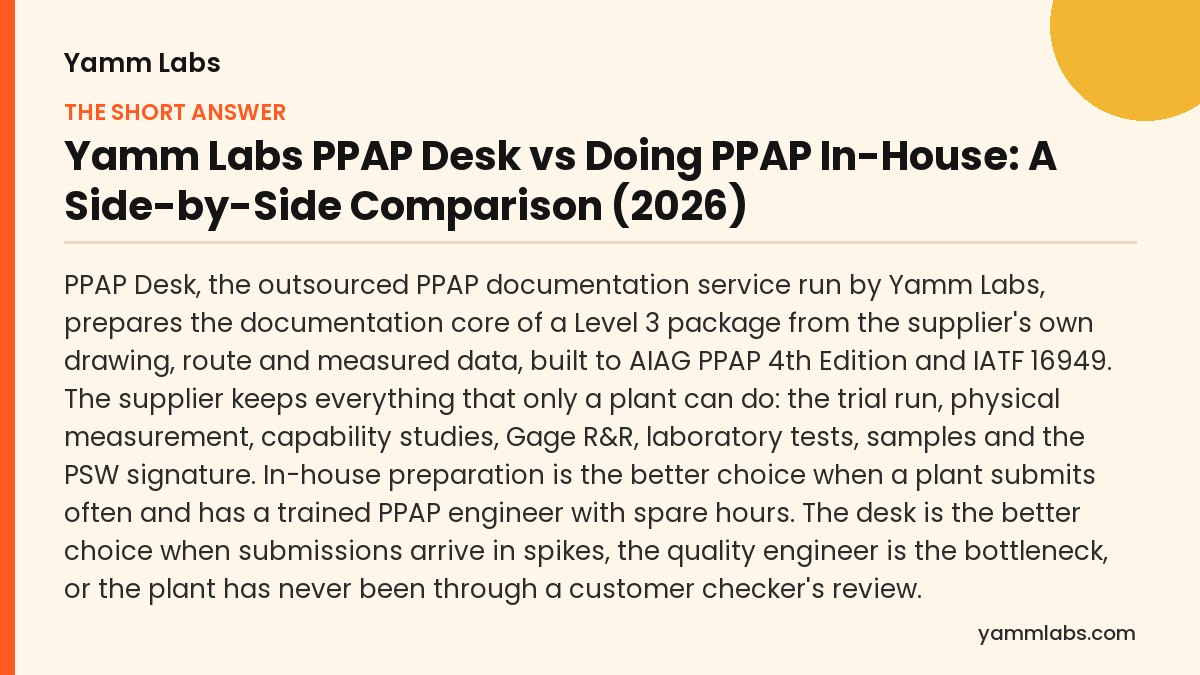
What does PPAP Desk actually do, and what does it never do?
The service takes five inputs from the plant: the released drawing, the confirmed process route, the gauge list, any customer-specific requirements or engineering change notes, and real measured data from the plant’s own trial. From those it builds one characteristic-to-operation map, then writes every document that can be authored from that map: the ballooned print and characteristic register, the Process Flow Diagram, the PFMEA and the Control Plan linked to it, the process and setup sheets, the checking-aid list and gauge specifications, the incoming inspection standard, the MSA, dimensional and initial process study formats, and a PSW draft with a package index.
Three things are outside the service by design. The desk never generates measurement data; every number in a dimensional report or capability study comes from the plant. It never runs the physical work: trial runs, Gage R&R trials, laboratory testing, samples, the master sample and IMDS entry stay with the supplier. And it never signs. The Part Submission Warrant is approved and signed by the supplier’s responsible official, because that authority cannot be delegated to a document provider under any customer’s requirements.
Under IATF 16949, which adopts ISO 9001, a document provider of this kind is an externally provided process under clause 8.4. The supplier defines the requirement, evaluates the provider, verifies the output and retains full responsibility for the submission. The PPAP Desk service page sets out the same division of labour in one line: the desk prepares, the plant’s quality team verifies, the responsible official signs.
PPAP Desk versus in-house: the side-by-side comparison
| Factor | PPAP Desk (outsourced documentation) | Doing PPAP in-house |
|---|---|---|
| Who authors the documents | The desk, from the plant’s drawing, route and data | The plant’s quality or APQP engineer |
| Who produces the evidence | The plant, always | The plant, always |
| Who signs the PSW | The supplier’s responsible official | The supplier’s responsible official |
| PFMEA to Control Plan linkage | Built from one characteristic map, so the two documents cannot drift apart | Depends on the engineer’s discipline and the templates in use |
| Speed on a new part | A two-part pilot runs on a five-day cycle from inputs to a checker-ready pack | Fast when the engineer is free; slow during launch spikes and audits |
| Cost model | No retainer, no software to install; the two-part pilot is free | Engineer hours, templates, training and the opportunity cost of documentation over defect prevention |
| Confidentiality | Drawings and data leave the plant under an NDA signed on day zero | Nothing leaves the plant |
| Customer-specific formats | Must be handed over with the inputs; the desk builds to the customer’s format | Easier when the team already knows the customer portal |
| Best fit | Small quality teams, launch spikes, first-time Level 3 submitters, many part numbers | Regular submission volume, a trained PPAP engineer with spare hours, sensitive designs |
Read the table for the pattern rather than the rows. The evidence, the ownership and the signature never move. What moves is the authoring of documents, and the question is only whether the plant’s engineer should spend hours formatting a PFMEA or spend them preventing the defect the PFMEA describes.
When is in-house PPAP the right call?
- You submit every month. A plant that runs PPAPs as routine already has templates, a trained engineer and a rhythm with its customer’s checker. Adding a desk adds a hand-off without removing work.
- The design is sensitive. Some customers restrict who may see the drawing. If the customer-specific requirements forbid external handling of the design record, the decision is made for you.
- The customer wants your engineer in the room. Where the checker expects to walk the line with the person who wrote the Control Plan, the author should be on the payroll.
- You are building permanent capability. A supplier moving from Tier-3 to Tier-2 status needs PPAP knowledge inside the plant, because the same people will run engineering changes, revalidations and corrective actions for years.
When does the outsourced desk make sense?
- The engineer is the bottleneck. If the quality engineer is measuring parts by day and formatting files by night, the documentation is what is slowing the submission, and that is the part a desk can take.
- Submissions arrive in spikes. New nominations, engineering changes and resubmission requests cluster around launches. A per-report service absorbs the spike without a hire.
- It is the plant’s first Level 3. First-time submitters lose weeks to structure: which element goes where, how the ballooned print numbers flow into the dimensional report, why the Control Plan must mirror the PFMEA line by line. A desk that has built the structure before removes that learning curve from the critical path.
- Many part numbers, one product family. When a family shares a route, one characteristic map serves the whole family, and the cost per report falls with each part.
Outsourcing the documents does not outsource the responsibility; the plant still measures, verifies and signs.
How does a PPAP Desk engagement run, day by day?
The pilot is deliberately small: two live parts, five working days, inside the plant’s existing quality process. Day zero is the NDA and the inputs. Day one confirms the route with the plant, because a PFMEA written against the wrong sequence of operations is worthless. Days two to four are the build and the desk’s own quality check, which walks every characteristic from the ballooned print through the Control Plan to the report formats. Day five delivers the checker-ready pack. The plant’s quality team then verifies each document against the shop floor, fills the evidence formats with its measured data, and the responsible official signs the PSW.
The commercial terms are on the service page: no retainer, a free two-part pilot, and nothing to install. The desk’s public case study is Manu Auto India, for which it has delivered more than fifty Level 3 PPAP reports in a consistent, indexed format built for the customer’s submission requirements.
What should a supplier ask before choosing either route?
Whichever way the decision goes, the same questions apply. Which of the eighteen elements will be authored, and which are the plant’s evidence? Does the author build to AIAG PPAP 4th Edition and to the customer’s specific requirements, including the customer’s own forms? How is the PFMEA linked to the Control Plan, and can that link be shown characteristic by characteristic? Who validates the capability calculations and the Gage R&R, and where does the raw data live?
What is the turnaround for one part and for a family, and how many revision cycles are included? For an external desk, add two more: who signs the NDA, and what is the data retention period after submission. The AI PPAP generator explainer lists the elements one by one and marks which are documents and which are evidence, which is the fastest way to scope any provider’s offer. For a broader set of buyer questions, the Questions Answered hub holds the PPAP set alongside the BFSI set.
A decision rule a plant manager can use
Outsource the documentation when the provider’s fee is lower than the cost of the engineer’s hours it replaces, plus the cost of the delay a late submission would cause, plus the cost of a rejection and resubmission. Keep it in-house when the plant has the hours, the templates and the customer relationship to absorb the work without slipping the launch. Most suppliers who run the arithmetic find the answer changes with the calendar: in-house in a quiet quarter, the desk during a launch. The service is built for exactly that pattern, which is why it is priced per report and carries no retainer.
A worked example: the Friday nomination in Manesar
Go back to the Tier-2 machining shop from the start of this article and run the decision rule on it. No new numbers are needed; the facts in the opening are enough.
- The inputs exist. The drawing is released, the route is confirmed and the gauges exist. Those are the inputs the desk needs on day zero, along with the customer’s requirements and, later, the plant’s measured data.
- The engineer is the bottleneck. The plant’s one quality engineer is already running a trial run for another part. Every hour spent formatting forty-odd pages is an hour taken from that trial.
- The work is a spike, not a routine. A new part number landing on a Friday, on top of a live trial, is the pattern a per-report service is built for.
On those facts the desk is the better route for this part. The NDA and inputs go over on day zero, the route is confirmed on day one, and the checker-ready pack arrives on day five. Meanwhile the engineer finishes the other trial, then verifies each document against the shop floor, fills the evidence formats with the plant’s own data, and hands the warrant to the responsible official to sign.
Change one fact and the answer can change. If the same shop were in a quiet quarter with the engineer free, in-house would be the sensible call. The rule follows the calendar, not a fixed preference.
Common mistakes when outsourcing PPAP documentation
Most problems with an outside desk come from the hand-off, not the drafting. These are the ones worth avoiding on the first order.
- Holding back the customer’s requirements. The desk builds to the customer’s format only if it has the customer-specific requirements and forms with the inputs. Sent later, they mean a rebuild.
- Skipping the route confirmation. A PFMEA written against the wrong sequence of operations is worthless. Confirm the route on day one, even when it feels obvious.
- Expecting the desk to supply numbers. Every figure in a dimensional report or capability study comes from the plant. A desk that offers to fill them in is a desk to avoid.
- Treating the pack as finished on delivery. The plant’s quality team still verifies every document against the shop floor before anything goes to the customer.
- Leaving confidentiality vague. Agree who signs the NDA and the data retention period after submission before the drawing leaves the plant.
- Not agreeing revision cycles. Ask how many revisions are included for one part and for a family, so a checker’s comments do not turn into a new negotiation.
How to brief a PPAP desk so the pack comes back usable
A good brief is short and complete. It gives the desk everything it cannot find out on its own and names the person in the plant who will answer questions.
- Send the released drawing and the confirmed process route.
- Send the gauge list, so the checking-aid list and gauge specifications match what the plant actually owns.
- Send the customer-specific requirements, the customer’s own forms and any engineering change notes.
- Name the submission level, which is Level 3 unless the customer says otherwise.
- Say which elements the desk should author and which the plant will supply as evidence.
- Name one contact in the plant for route questions and one person who will verify the pack.
- Agree the dates: inputs on day zero, route confirmation on day one, checker-ready pack on day five.
With that brief, the desk can build one characteristic map and write the pack from it. Without it, the first two days go on questions. PPAP requirements and customer manuals change over time, so confirm the current text with your compliance team or the customer’s supplier quality contact before each new programme.
People also ask
Can a Tier-2 supplier outsource PPAP documentation under IATF 16949?
Yes. Neither the AIAG PPAP manual nor IATF 16949 requires supporting documents to be authored in-house. External preparation is an externally provided process under clause 8.4 of ISO 9001, which IATF 16949 adopts, so the supplier controls the provider and retains full responsibility for the submission.
Does PPAP Desk sign the Part Submission Warrant?
No. The PSW is signed by the supplier’s responsible official and approved by the customer. The desk prepares a PSW draft and the package index; the authority to warrant the part never leaves the plant.
Does the desk produce the dimensional and capability data?
No. The desk provides the ballooned report and study formats; the plant measures the parts, runs the Gage R&R and the initial process study, and enters its own data. No synthetic data is ever generated.
What does an engagement cost and how long does it take?
The two-part pilot is free, with no retainer and no software to install. It runs on a five-day cycle from the NDA and inputs to a checker-ready pack.
Is PPAP Desk a software tool?
No. It is a documentation service, so there is nothing to install. The desk works from the plant’s drawing, route, gauge list, customer requirements and measured data, and returns a checker-ready pack for the plant to verify and sign.
Can PPAP Desk handle a whole product family?
Yes, and families are where it works best. When several part numbers share a route, one characteristic map serves the whole family, so the PFMEA, Control Plan and report formats stay consistent across parts and the cost per report falls with each part added. The plant still measures and signs for every part number.
Deciding between a desk and a hire before the next launch?
Prove it on two live parts: a five-day pilot inside your existing quality process. No retainer, no software setup. Start a 2-part pilot →
One Comment